Related Topics:
Variable Frequency Drive Inspection-
How to use a communication optical cable inspection instrument
Conducting a visual inspection test involves using a fiber scope or microscope to examine the endfaces of connectors for dirt, scratches, or cracks. Always inspect before you connect. Cable contamination can also damage your equipment, turning a preventive measure into an expensive. Fiber optic cable is a type of cabling that contains one or more optical fibers for transmitting data at high speeds and/or over long distances using light. These fibers are most commonly made of glass and are very thin, typically less than a tenth of the width of a human hair. Before diving into the testing process, it's crucial to understand why testing is necessary. Cable contamination can also.
-
Network Cabinet Potential Inspection Report
Use this network cabinet inspection checklist to capture cabinet IDs, PDU and UPS details, fiber patch panels, and structured cabling for site audits safely. It covers things like hardware, software, user access, and security settings to find issues or risks. What's in our Audit a Network Checklist white paper: What is a Network Audit? Why. As an MSP, your role is to ensure your client's network operates without a hitch. You may have a requirement to re-locate or upgrade data cabinets to create more space or facilitate the installation of additional equipment.
-
Cable tray inspection report
Use this Cable Inspection Checklist to complete inspections from your mobile device, fill out forms in the field, attach photos/videos, sign off digitally, and export or share as CSV/Excel and PDF. Open ends plugged not Cable tray, sharp edge, burr etc. damaged during construction period. Support type / size / welding / anchoring. Expansion joints as shown on drawings. The process described here takes a systematic approach to ensuring that cable tray installations meet safety, reliability, and project-specific needs while following to. Cable trays play a crucial role in ensuring the safety and efficiency of electrical and communication systems. With their responsibility to manage cables effectively, their inspection is essential to maintaining stable performance and meeting design standards. The cost of this template that is less than the cost of an hour of your time. Need to maintain cables safely? Don't want. This article is about ITP (Inspection Test Plan) Plan for Cable Tray and Accessories Installation.
[PDF Version]
-
Pakistan Fiber Optic Endface Inspection Instrument Remote Monitoring Type
The FIP100 from Tempo is a fully automated inspection tool that provides fast and reliable analysis of fiber optic connector end faces and bulkheads. Since contamination or damage to the fiber end face can lead to signal attenuation, reflection loss, and unreliable connections, regular inspection and cleaning of the fiber end. AFL Fiber Inspection Products enable network technicians and other personnel to safely inspect fiber endfaces for contamination and verify the effectiveness of fiber cleaning procedures. 📦 For purchasing, use the RP Photonics Buyer's Guide for fiber endface inspection. Fiber loss and OTDR testing can expose this problem, but in many cases, dirty.
-
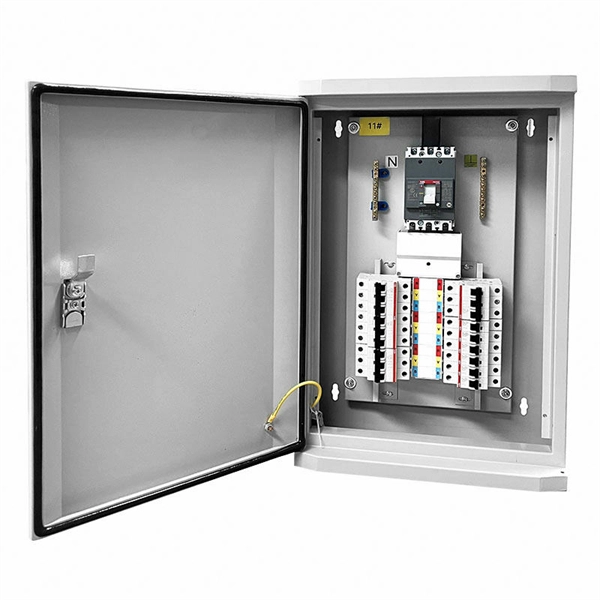
Inspection sequence of relay protection devices
A comprehensive testing program should simulate fault and normal operating conditions of the relay. Setting determines pick-up value/time. Tests are conducted by the manufacturer at manufacturer s works, and by the user at site during commissioning and periodic maintenance. These tests are further divided into. The testing and verification of relay protection devices can be divided into four groups: Type tests are needed to prove that a protection relay meets the claimed specification and follows all relevant standards. Since the basic function of a protection relay is to correctly function under abnormal. The first relays were Electromechanical (EM): machines with moving parts actuated by coils connected to current and voltage sources. 15 seconds in its 30+ year life. But failure to operate as intended can result in extensive damage, extended power outages, and loss of life.
[PDF Version]
-
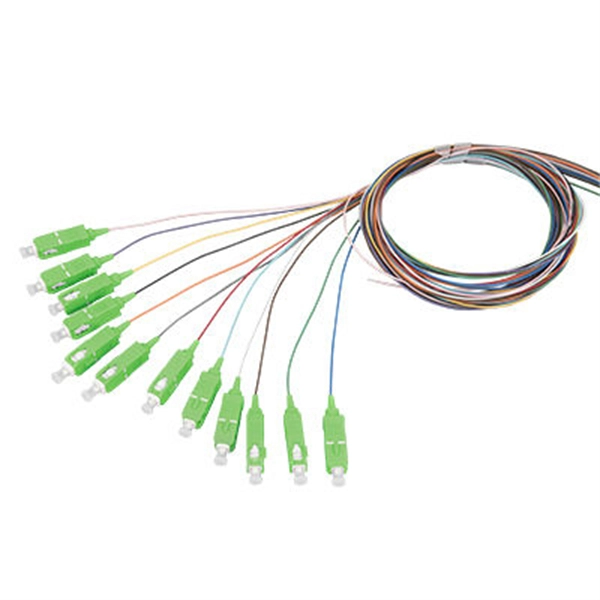
Optical module to FC hard drive interface
Moving the HDD controller from the interface card to the disk drive helped to standardize the host/controller interface, reduce the programming complexity in the host device driver, and reduced system cost and complexity.Overview are accessed over one of a number of types, including (PATA, also called IDE or ; described before the introduction of SATA as ATA), (SATA),, (SAS),. The earliest hard disk drive (HDD) interfaces were bit serial data interfaces that connected an HDD to a controller with two cables, one for control and one for data. An additional cable was used for power, initi. Historical Word serial interfaces connect a hard disk drive to a bus adapter with one cable for combined data/control. (As for all early interfaces above, each drive also has an additional power cable, usually direct to the power s.
[PDF Version]